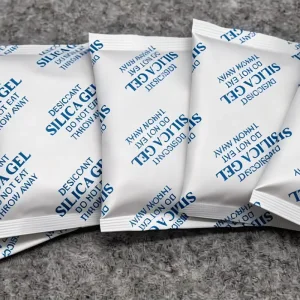
Optimized for severe humidity control across North African industrial hubs including Annaba port logistics.
Annaba, as one of Algeria's premier industrial and port powerhouses, experiences distinct Mediterranean climatic conditions marked by high relative humidity and saline coastal air. These environmental factors pose significant risks to metallurgical exports, steel manufacturing, chemical storage, and containerized maritime shipping. Our advanced desiccant technology acts as the ultimate defensive line against container rain, mold, rust, and product degradation.
Designed specifically for ocean freight departing from Annaba port, preventing container sweat and structural moisture damage during long Mediterranean and global voyages.
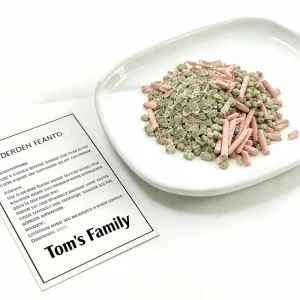
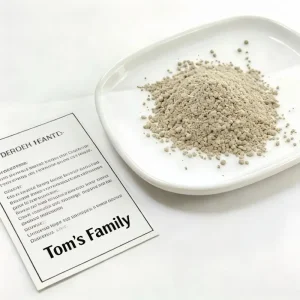
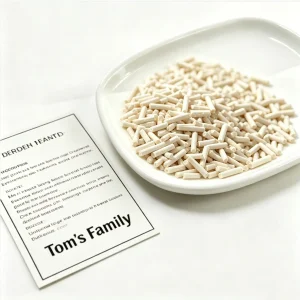
Utilizing high-purity montmorillonite clay, activated carbon, and specialized polymer binders to lock moisture safely without leakage risks.
Tailored sizing, high-density packaging, and customized private labeling to seamlessly integrate with regional industrial distribution demands.
Tom's Family team is a leading global manufacturer and a key member of the Shengyu Group. With the aid of standardized production, an exceptionally experienced sales force, advanced laboratory testing facilities, and prompt global delivery, we have successfully catered to the rigorous demands of international markets, establishing ourselves as a top-ranking industrial desiccant and absorbent factory worldwide.


"We deliver healthy, comfortable, and sustainable protection solutions." Through continuous material innovation, eco-friendly manufacturing, and rigorous quality control, we ensure global supply chain integrity for partners in Annaba and beyond.
In response to global industrial shifts towards carbon neutrality and circular economies, our R&D division has pioneered next-generation biodegradable desiccant packaging and high-efficiency mineral formulations. By optimizing moisture adsorption kinetics and reducing carbon footprints during manufacturing, we empower industrial clients in Annaba to achieve sustainable operational goals without sacrificing performance.
Upgrading raw mineral selection to maximize surface area and boost low-temperature moisture intake efficiency by over 25%.
Developing color-changing indicator integration for real-time saturation monitoring inside sealed industrial machinery and shipping containers.
Introducing fully recyclable, compostable non-woven outer casing materials designed to eliminate industrial plastic waste entirely.
Explore our complete manufacturing catalog designed to meet diverse industrial, commercial, and consumer requirements.
Take a virtual walkthrough of our state-of-the-art manufacturing plants, automated packaging lines, and rigorous quality inspection laboratories.
Expert insights into sourcing industrial desiccants and establishing direct supply chains for the Annaba market.
Annaba's Mediterranean coastal climate features high relative humidity and temperature fluctuations. During container transit, temperature drops cause "container rain" (condensation), leading to severe corrosion, mold, and packaging failure. Our high-capacity desiccants absorb excess moisture rapidly, protecting your valuable cargo throughout the journey.
Yes. As a leading manufacturer under Shengyu Group, we offer comprehensive OEM and ODM services, including customized grammage, specialized non-woven wrapping materials, multi-language branding, and tailored carton configurations to match your market positioning.
Our manufacturing processes strictly adhere to ISO9001 quality management standards, REACH regulations, RoHS compliance, and DMF-free safety certifications, ensuring complete safety for industrial, commercial, and household applications.
You can instantly connect with our international trade team by clicking the "Send Inquiry Now" button below or visiting our contact page. We offer prompt sample dispatch and competitive shipping quotations tailored to North African ports.
 TOM'S FAMILY